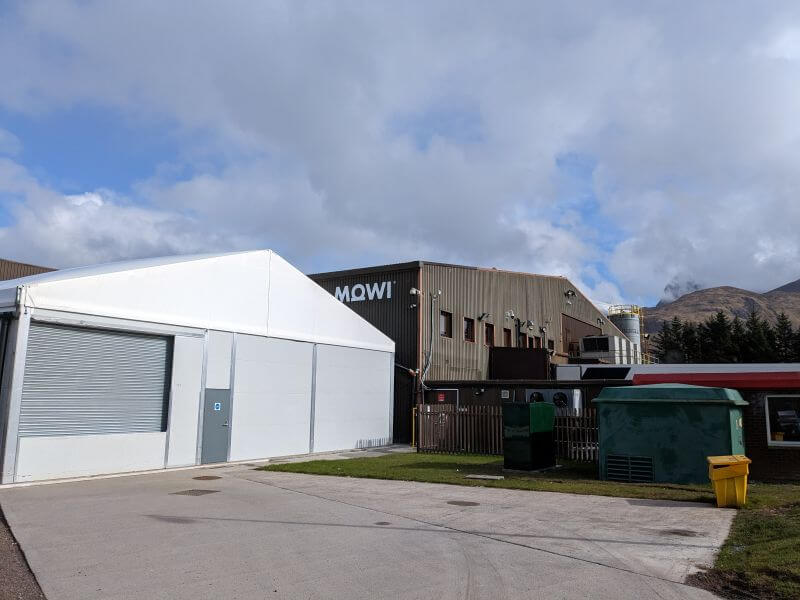
HF was entrusted with the design, installation and delivery of Mechanical & Electrical Services for MOWI’s advanced processing facility in Fort William, a key location in MOWI’s operations. The ‘Stage 1’ extension to their facility required a ground up installation of mechanical and electrical systems for the facility that processes and packages seafood. This meant that it required a highly reliable and scalable electrical infrastructure, as well as efficient and secure mechanical and automated systems. With vast experience in delivering complex projects across various industries, HF was ideally positioned to meet these needs and exceed MOWI’s expectations.
The scale and complexity of the project required HF’s expertise in a wide range of services. From electrical distribution systems to plumbing & mechanical systems as well as automated control systems. HF provided a fully integrated solution. This multifaceted approach allowed MOWI to benefit from a single point of contact for all electrical and mechanical services, ensuring smooth coordination and a streamlined installation process working alongside MOWI’s chosen third party contractors.
The electrical infrastructure was designed to meet the high power demands of the facility, supporting a range of operations, from processing machinery to environmental controls. HF installed a 1600A Schneider Main Panel Board on the first floor, which was directly connected to a 1250A supply in the main switch room on the ground floor. This centralised system ensures that power is distributed efficiently and reliably across the site, minimising the risk of outages or inefficiencies. Surge protection devices (SPDs) were incorporated into all main and local distribution boards to safeguard critical equipment from electrical surges, which are common in industrial settings, preventing costly downtime and ensuring the longevity of the equipment.
The installation of a robust and flexible distribution system was crucial to meeting the diverse needs of the facility. HF’s engineers designed a customised network of power outlets, data ports, and distribution boards to serve key areas, including the vacuum room, comms room, box store, external areas, car park and the dispatch robotics system. Each section was carefully mapped to ensure the system was scalable and adaptable for future upgrades. This foresight ensures that as MOWI expands or introduces new technologies, the electrical infrastructure can accommodate those changes with minimal disruption.
A significant benefit of this customised system is the ability to quickly implement new equipment or systems without requiring major overhauls or rewiring. The facility can grow and evolve into phase two of the project which we are actively involved in, without incurring significant additional costs or time delays. The secondary section panel board, positioned in ceiling voids, ensures that routine maintenance and system upgrades can be carried out with ease, reducing operational disruptions.
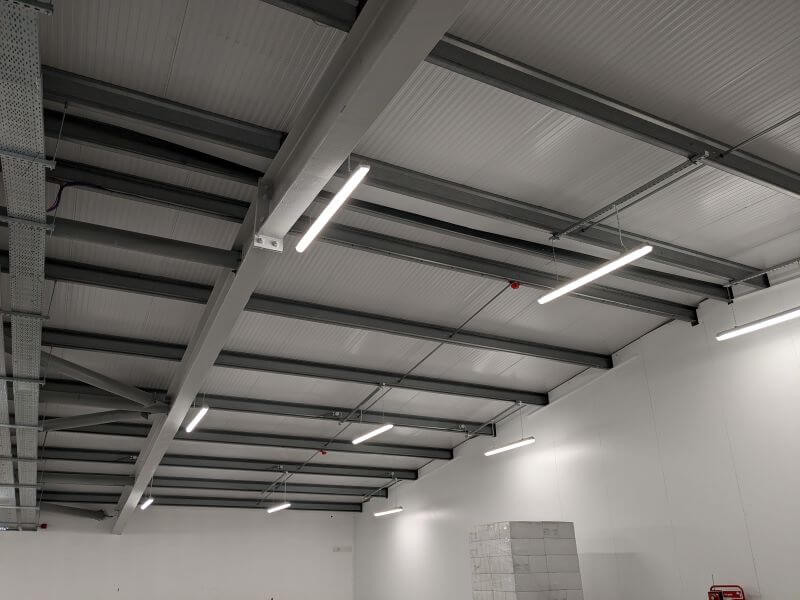
HF took extra care in designing and installing industrial-grade containment systems. These included ladder racks and cable trays of various sizes to manage and protect cables, which are essential for the safe operation of the facility. These systems were carefully mapped to avoid interfering with workflow and ensure that they could handle the ongoing expansion of equipment. In areas where cables would be exposed to high traffic or potential damage, galvanised and PVC conduits were used to further safeguard the electrical infrastructure. This proactive approach in cable management prevents the risk of system failures caused by wear and tear, reducing the long-term maintenance costs for MOWI.
Efficient lighting systems were a key component of the facility’s design. HF installed LED lighting across the entire site, ensuring high-efficiency illumination that reduces energy consumption while maintaining optimal working conditions. The use of LED lighting means MOWI will benefit from long-term energy savings and a significant reduction in ongoing maintenance costs, as LEDs have a longer lifespan compared to traditional lighting systems.
Emergency lighting circuits were installed throughout the facility, with strategically placed key switch panels for easy testing. This automated system ensures that MOWI meets all safety and regulatory requirements, while also providing a clear and accessible method for verifying the system’s integrity. Passive infrared (PIR) sensors were incorporated into corridors and stairwells to automatically control lighting, further enhancing energy efficiency. By reducing unnecessary energy use in low-traffic areas, MOWI can realise substantial savings on electricity bills.
Given the critical role of communication systems in any industrial setting, HF installed a comprehensive data network throughout the facility. The installation included high-speed CAT6A cabling and an OM3 fiber optic backbone, ensuring fast, secure, and reliable communication across the site. Wi-Fi access points and additional data ports were installed in key locations to support the connectivity needs of employees and equipment.
Importantly, the data system was designed with future scalability in mind. MOWI’s facility is poised for growth and the communication infrastructure can be easily expanded to accommodate new systems, equipment, and digital technologies. This scalability future-proofs MOWI’s investment, enabling the company to adapt to emerging technologies without significant new capital expenditures or disruptions to operations.
Our Mechanical Division was pivotal in the successful delivery of MOWI’s processing facility, implementing essential systems that enhanced operational efficiency, supported production processes and provided a comfortable and functional environment for employees. The tailored solutions were designed with reliability, energy efficiency and scalability in mind, ensuring the facility could meet both its immediate operational demands and its future growth needs.
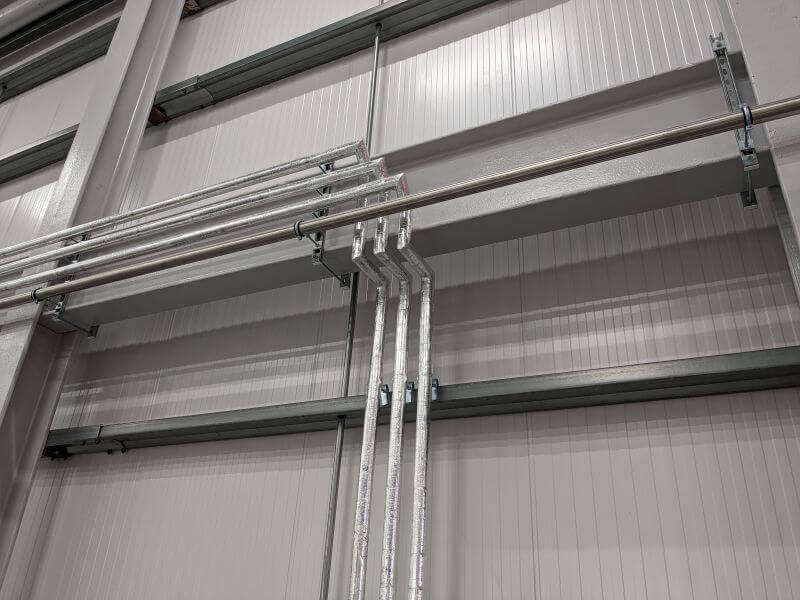
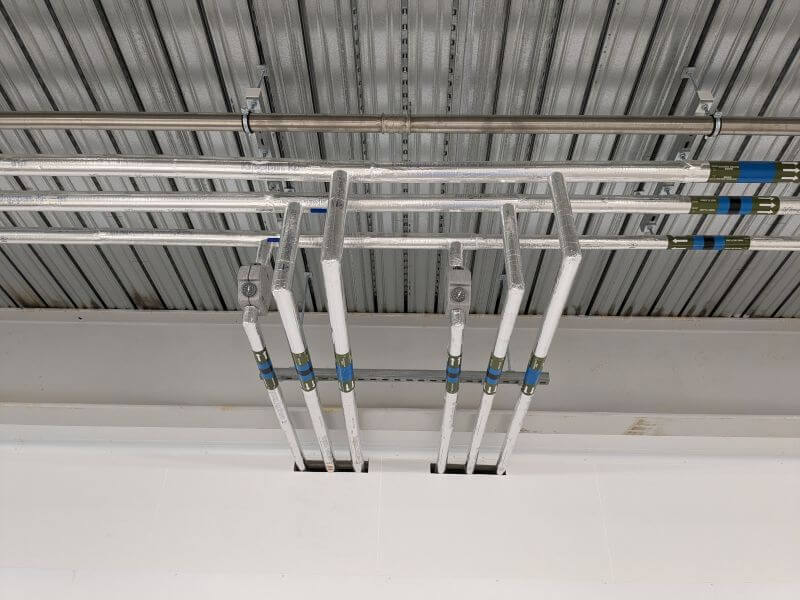
A central aspect of the project was the installation of compressed air lines, which play a critical role in powering machinery and automation systems integral to seafood processing. These lines were carefully designed to ensure reliability and reduce the risk of downtime, which is vital in a high-output facility like MOWI’s. Similarly, HF installed a processed water system that delivers a consistent and efficient water supply tailored to the production requirements. This system was designed with scalability, enabling MOWI to integrate new equipment or increase capacity without major modifications.
To enhance energy efficiency, HF implemented a heat recovery ventilation system that captures and reuses waste heat from production processes. This not only reduces energy consumption but also improves the indoor environment for employees by maintaining air quality. Alongside this, HF installed air conditioning systems to provide precise climate control, ensuring that the facility meets the strict temperature requirements necessary for seafood processing while maintaining comfortable conditions in administrative and communal areas.
The facility’s heating systems were seamlessly integrated with the HVAC infrastructure to provide consistent and energy-efficient warmth. HF also delivered comprehensive installations for toilets, changing rooms, and kitchen areas, ensuring that the workforce had access to modern, hygienic facilities that support their well being. These spaces were designed to accommodate the high volume of employees and improve the overall workplace environment.
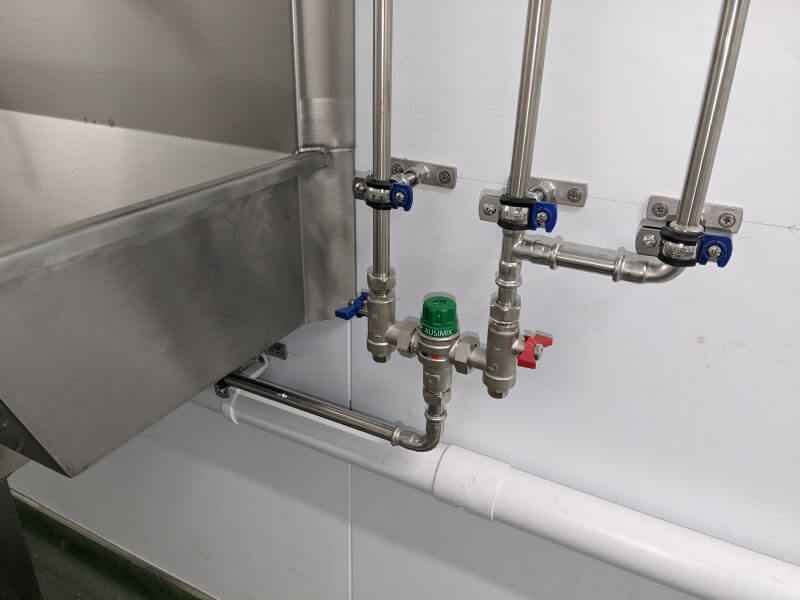
Another critical aspect was the design and installation of the water services and drainage systems, which are essential for supporting the new functions of the building. These systems were constructed to handle high usage and adhere to stringent hygiene standards required in the food processing industry. Additionally, HF developed a hot water system capable of meeting the facility’s demanding requirements, particularly in cleaning and sanitation areas, ensuring compliance with industry regulations and supporting uninterrupted production schedules.
Throughout the course of the project, HF encountered several unique challenges, particularly given the live-production environment and the requirement for minimal downtime during installation. Coordinating with MOWI’s operations team, HF was able to plan phased power isolations and carry out installations at optimum times to prevent disruptions. This level of flexibility was critical to ensuring the project remained on schedule and did not affect MOWI’s production timelines.
Another challenge was the harsh environment within certain processing areas, which required specialised equipment and materials. For example, areas prone to high humidity and moisture were equipped with IP-rated outlets and stainless-steel lighting fixtures to ensure durability and functionality in these demanding conditions. HF’s ability to anticipate these challenges and design solutions that were both cost-effective and resilient was a key factor in the success of the project.
HF’s commitment to safety and regulatory compliance was evident throughout the entire project. From the initial design phase to final testing and handover, HF adhered to all necessary safety standards, including the latest BS7671 wiring regulations and the Electricity at Work Regulations (1989). The project was also thoroughly documented with risk assessments and detailed Operations and Maintenance (O&M) manuals. These documents ensure that MOWI has a comprehensive guide to safely maintain and operate all installed systems.
One of the greatest advantages MOWI gained from partnering with HF was the seamless integration of services across disciplines. Instead of working with multiple contractors for the range of services that we provided, MOWI had the benefit of a single point of contact for all areas of the project. This unified approach saved time, reduced the risk of miscommunication, and ensured that the entire system functioned as one cohesive unit.
The result is a state-of-the-art facility with enhanced operational efficiency, greater energy savings, and a long-term, scalable infrastructure capable of supporting future growth. MOWI is now equipped with a future-proof solution that not only meets its current needs but also accommodates future expansions without the need for costly upgrades or downtime.
Through this project, HF demonstrated its ability to deliver a comprehensive, integrated solution tailored to the specific needs of MOWI’s facility. With a focus on safety, efficiency, and scalability, we have helped MOWI enhance its operations, reduce costs, and future-proof its infrastructure for continued growth. The seamless integration of services underscores HF’s strength as a leader in providing complete, customised solutions to industrial clients.



From technical insights to our latest project updates, stay connected with everything going on at HF.